JoeisaRobot
Explore our premium range of commercial coffee hardware, self-serve automated kiosks, and advanced temperature-controlled dispensers.
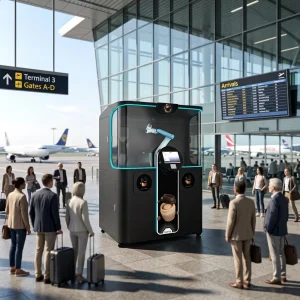
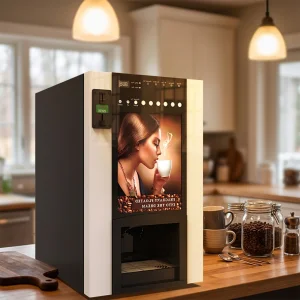
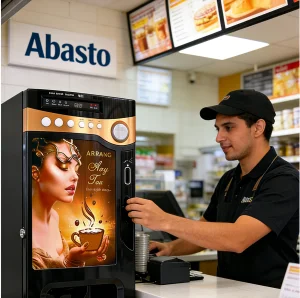
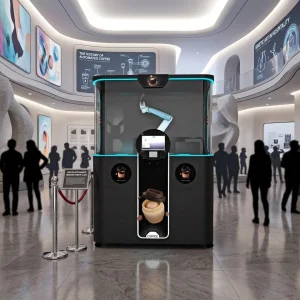
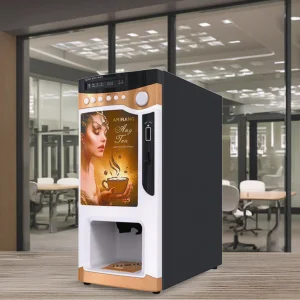
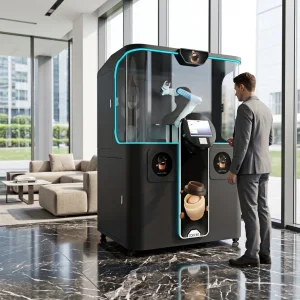
In high-throughput hospitality and corporate retail environments, maintaining the sensory integrity of brewed coffee is dependent on exact temperature regulation. Whether through custom-manufactured vacuum-insulated coffee thermos vessels or industrial heat exchange elements inside fully automated dispensing kiosks, preventing thermal degradation is key. Thermal degradation shifts flavor profiles by accelerating oxidation and structural compound breaking.
As an ISO9001 certified OEM/ODM manufacturing partner, we specialize in high-efficiency thermal retention solutions. We utilize double-wall SUS304/SUS316 stainless steel vacuum gaps combined with low-emissivity copper plating to minimize radiant heat transfer. By combining mechanical temperature containment with computerized heat controllers, our commercial systems deliver hot drinks consistently at the standard 80°C hot extraction target. This design delivers reliable performance, cup after cup.
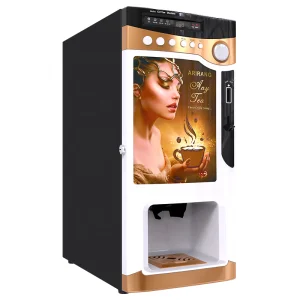
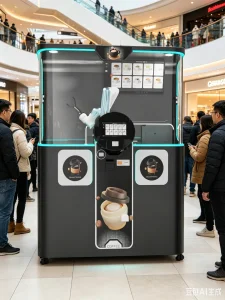
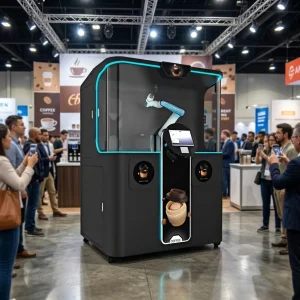
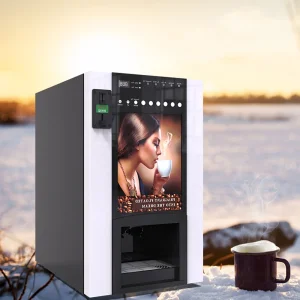
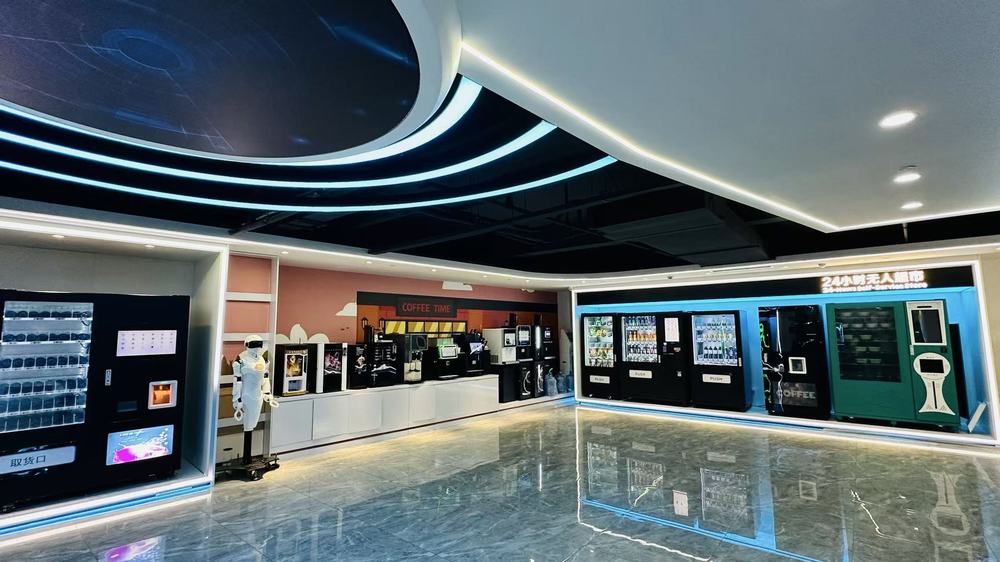
From desktop coin-operated coffee machines to multi-axis robotic arms preparing artisan fresh-ground espresso, we offer flexible OEM solutions. We supply key thermal components, mechanical parts, custom software integration, and completed machinery configurations tailored to your brand's specifications.
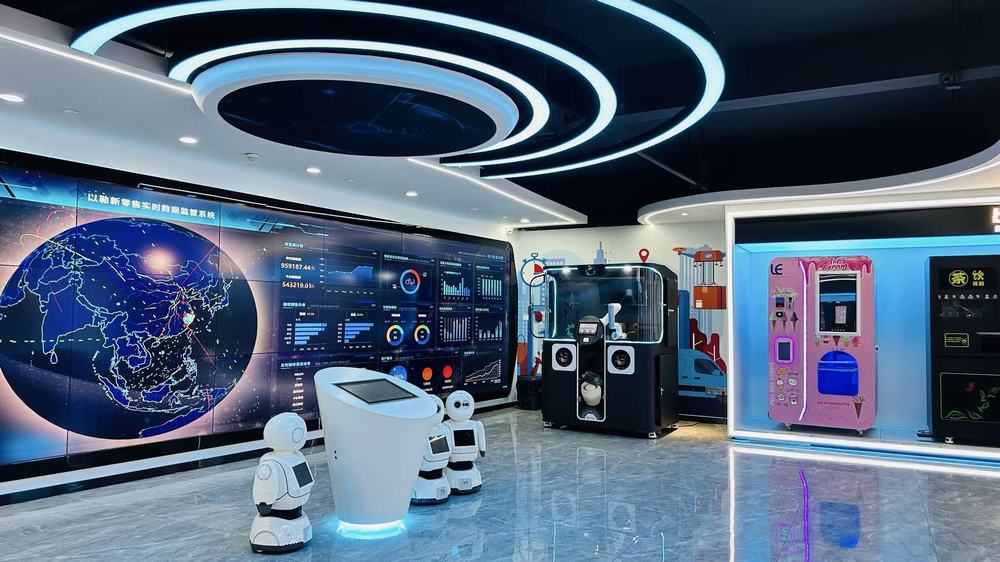
Verified manufacturing capacities, compliance standards, and product quality controls based on 19 years of global export experience.

Developing next-generation thermodynamic retention systems and IoT integrated beverage delivery platforms.
Our material science engineers are testing specialized anti-scaling coatings for copper-lined vacuum chambers. These materials maintain thermal efficiency in regions with high calcium and magnesium content in local tap water. This improvement extends system lifespan by up to 40%.
We are integrating micro-thermoelectric heating zones along the internal dispensing lines. Controlled by PID feed-back logic, this system ensures the first cup is served at the exact temperature target, even after long standby periods, minimizing early-cup heat loss.
Our upcoming generation of high-capacity kiosks features cloud diagnostics. Smart sensors monitor thermal performance, pressure levels, and flow rates in real time. Systems automatically alert fleet managers before component wear impacts drink quality.
How our manufacturing center in China delivers cost-efficiency, consistent quality, and reliable export fulfillment.
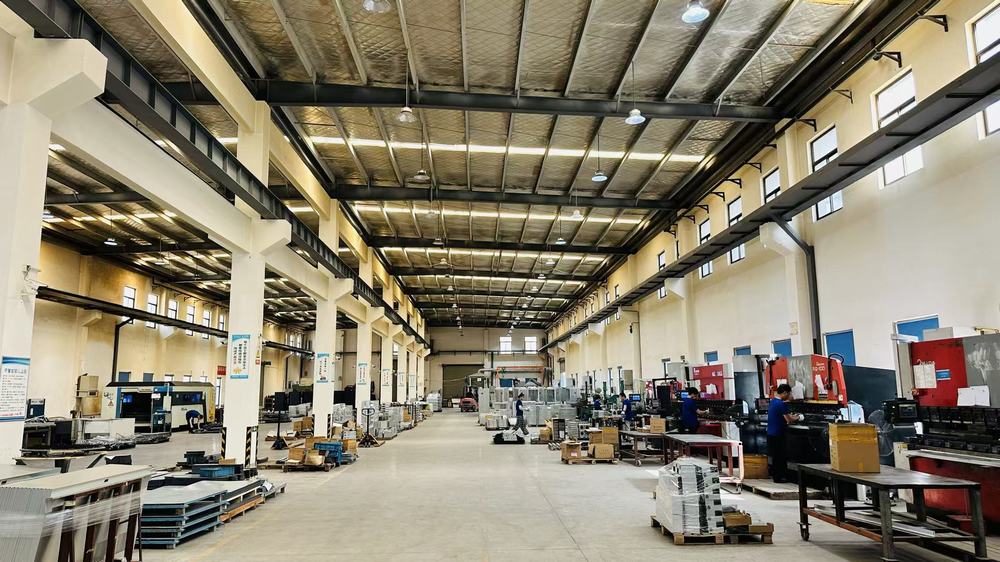
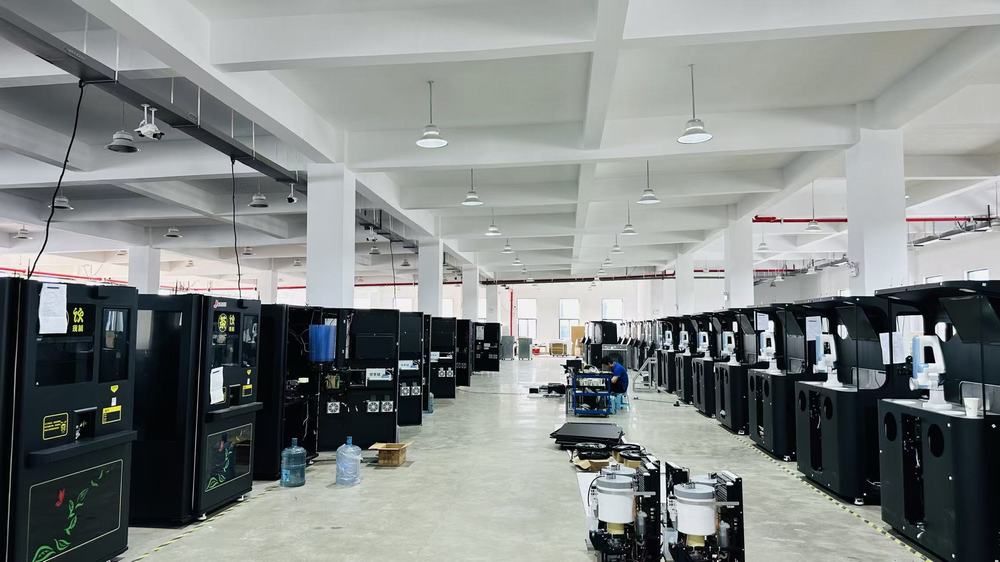
Our facility operates 6 high-precision assembly lines that group sheet-metal stamping, vacuum brazing, powder coating, and electronic wiring into a single workflow. Operating out of our 32,496 square meter plant, we manage the production process in-house, minimizing reliance on outside component suppliers. This integration reduces delays and ensures consistent build quality.
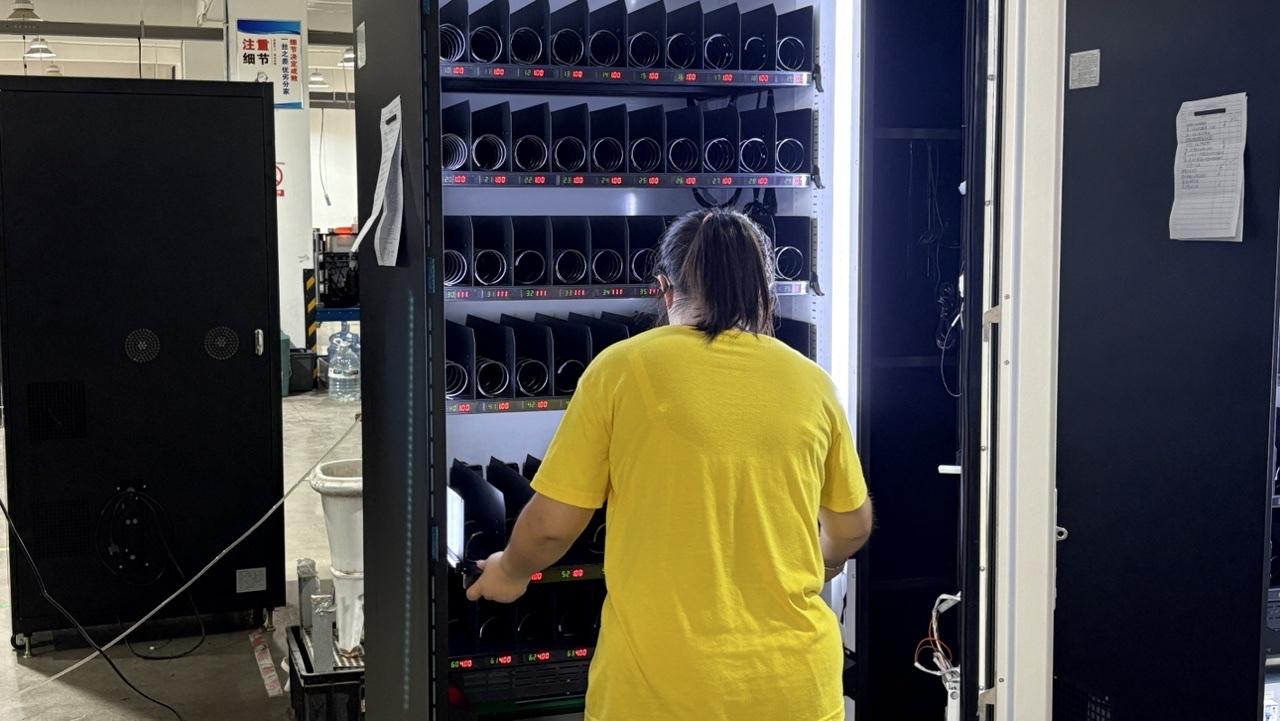
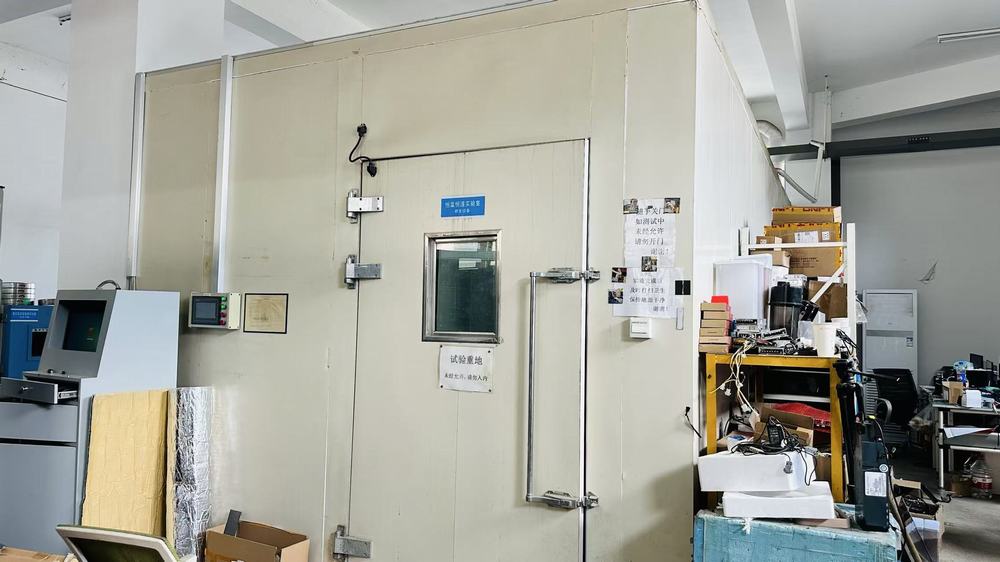
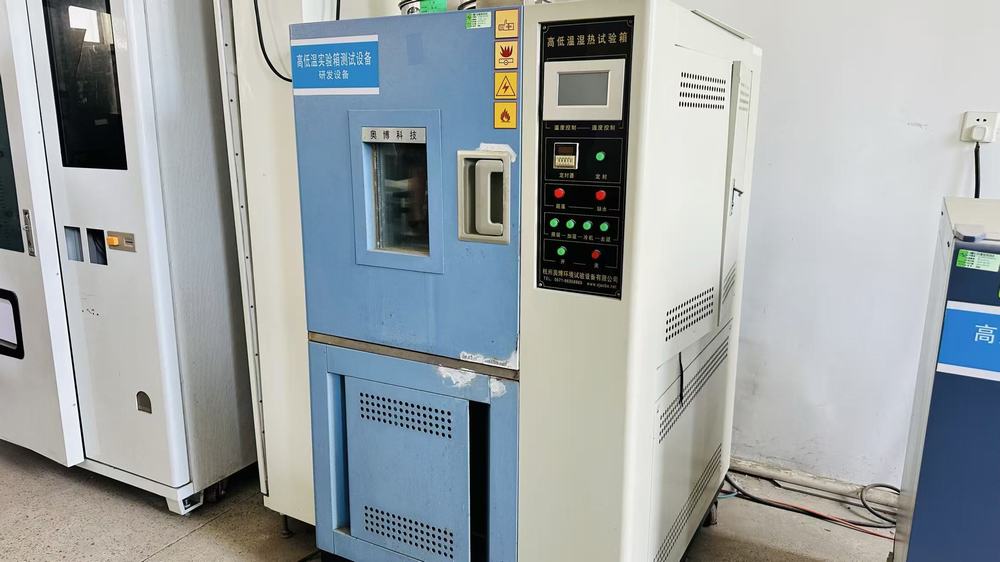
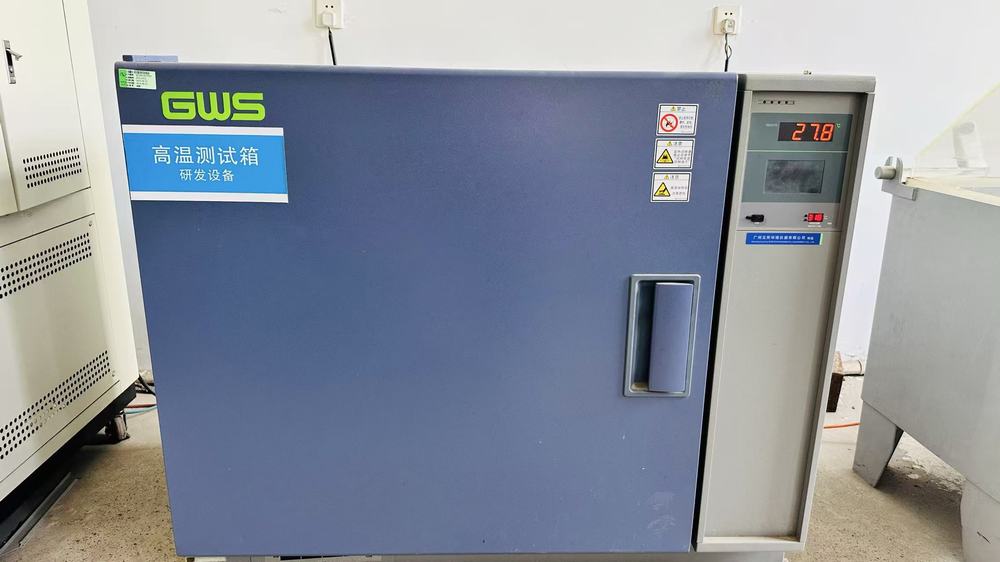
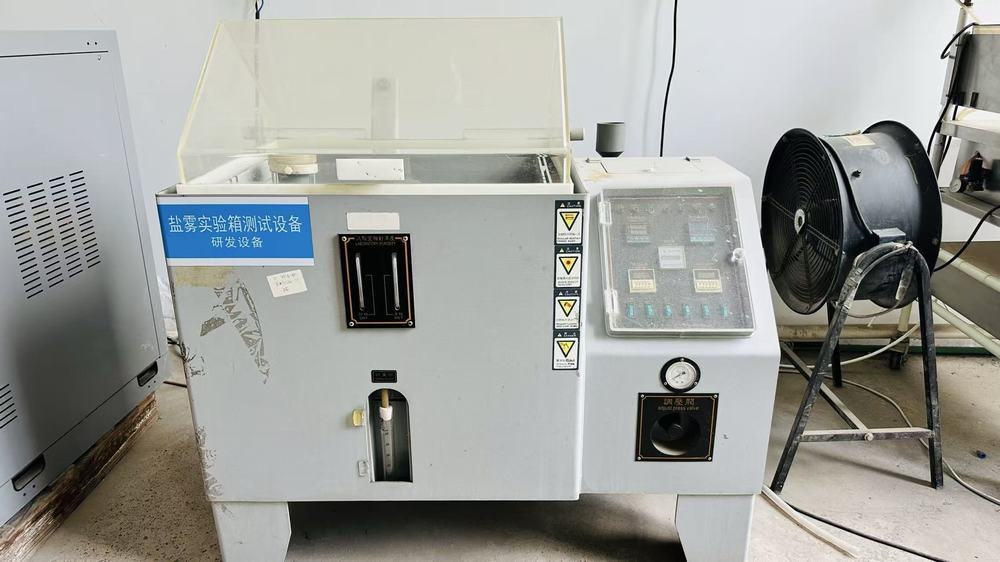
Every product undergoes strict QC testing before shipping. This process includes structural vacuum leak checks, pressure tests, and electrical safety diagnostics. This strict quality control is the foundation of our CE, ISO9001, and IEC 60335 certifications.
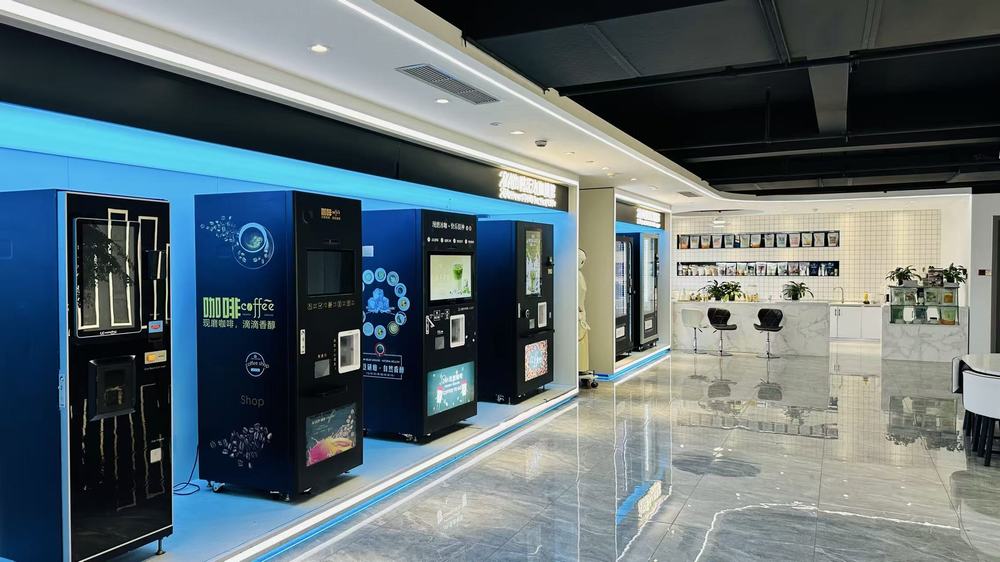
Custom engineering solutions tailored to meet the needs of international retailers, corporate brands, and bulk wholesalers.
We provide custom color coatings, silk-screened logos, customized UI layouts, and bespoke product enclosures to match your brand identity.
Our electronic dispensing platforms support external payment systems, corporate intranet cards, and customized telemetry dashboards.
We build products to meet national electrical safety, food-contact material (FDA/LFGB), and environmental standards, simplifying customs clearance.
Take an inside look at our 32,496 square meter production facility, advanced testing labs, and assembly workshops.
Clear, direct answers regarding customization capabilities, MOQ parameters, compliance frameworks, and logistics.
Review our full inventory of fresh-ground systems, coin-operated tabletop units, and specialized beverage makers.